Corrosion Allowance or Coating: 5 Design Options for Steel in Acid Gas Service
 Edita RojasovaLast Updated: Oct 27, 2026
Corrosion Allowance vs Coating: Key Points
- A corrosion allowance is extra steel thickness that corrosion is expected to consume over the design life; it only works when metal loss is predictable and reasonably uniform.
- Acid condensate attack concentrates at cold spots, air in-leakage points and under retained deposits, so an allowance can be consumed locally long before the average wall is thin.
- Coated carbon steel keeps condensate off the steel; Polylloy grades are matched by service limit, from CorrosionGard®-160S at 160 °C to FlueGard®-225SQC at 225 °C and FlueGard-455CHT at 455 °C (850 °F).
- Allowance plus coating is a design combination in which the coating keeps acid off the steel and the allowance holds structural margin if the film is damaged between inspections.
- 316L, higher alloys and thin stainless liners remain right where steel cannot be blasted, coated or inspected, but added liner thickness does not remove pitting or crevice corrosion.
- A design review accepts protected carbon steel on evidence: the expected corrosion mechanism, conditions at the metal surface, bulletin data, test reports with their limits, comparable field references and an inspection plan.
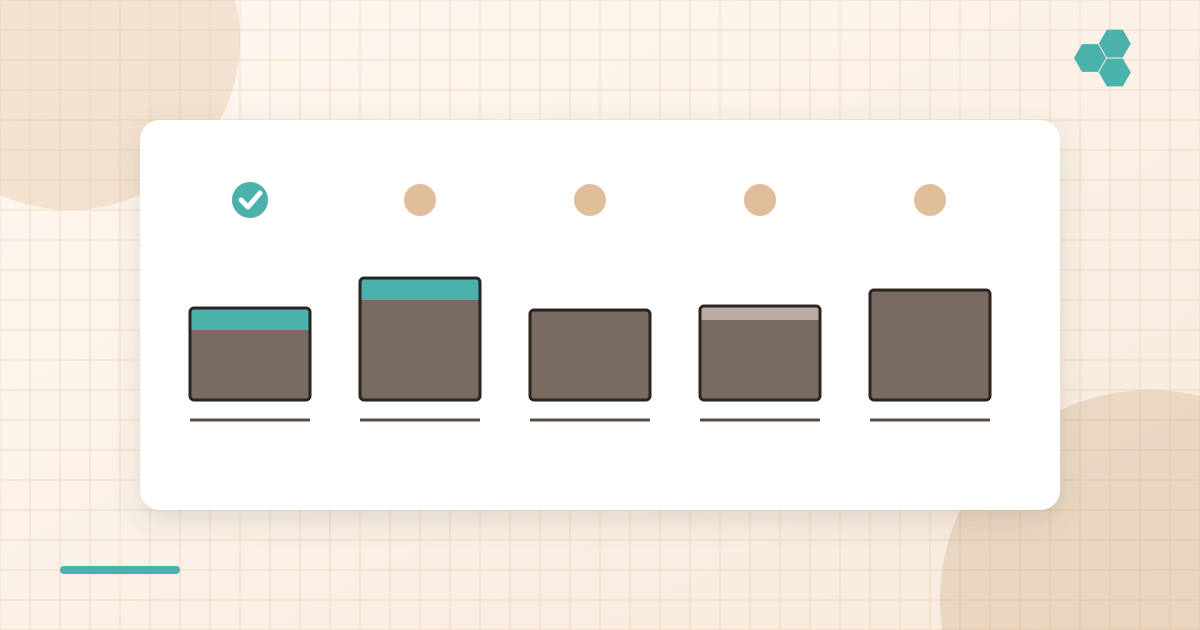
Decide by the corrosion mechanism you expect: a corrosion allowance only buys time against predictable, uniform metal loss, while acid condensate attacks carbon steel at cold spots, seals and deposits. Five design options are compared here: coated carbon steel, allowance plus coating, solid 316L or higher alloy, a stainless liner, and bare steel with allowance.
Corrosion Allowance and Coating as Design Choices for Acid Gas Steel
Corrosion allowance and coating are two different answers to the same design question: how carbon steel in acid flue gas service survives its design life. One sacrifices thickness; the other keeps the acid off the steel.
What a Corrosion Allowance Assumes
A corrosion allowance is extra wall thickness added to steel beyond what strength requires, set by the designer or engineer of record to be consumed by corrosion over the equipment's design life. The value and its code basis are project decisions, and this page gives none.
The approach works when metal loss is predictable and roughly uniform. Polylloy's technical paper on stainless steels and claddings warns that a low average corrosion rate can hide a penetration risk, which is the weak point of any allowance sized on average loss.
Why Acid Gas Service Breaks That Assumption
Acid condenses where steel runs below the acid dew point, typically 120 to 160 °C in cement plant flue gas depending on sulfur trioxide (SO3) and moisture (International Cement Review (ICR), May 2026). That happens at cold spots, at air in-leakage around doors and expansion joints, and during shutdowns, as the acid dew point corrosion warning signs show.
The technical paper describes the sequence: deposition in operation, cooling at shutdown, moisture uptake, salt dissolution, then localized corrosion beneath retained deposits. Loss is local, so the allowance is consumed at the worst detail, not across the wall.
Selection Criteria Used to Rank the Five Steel Design Options
Each steel design option was assessed against five criteria:
- Tolerance of localized acid and chloride condensate attack.
- Fit to the temperature envelope, including excursions.
- Whether it can be fabricated, prepared and inspected on the actual geometry.
- What an inspection can verify, such as wall thickness or film continuity.
- Evidence available for a design review.
The order reflects fit to the stated duty: steel in acid gas service with condensation risk. A coated option ranks first on that duty match, and each lower entry states where it is the right answer.
Five Steel Design Options for Acid Gas Service at a Glance
The table compares the five options in the order they are described; UT means ultrasonic thickness testing and DFT means dry film thickness. Cost basis is project-specific on every row.
| Design option | Protects by | Main failure risk | Verified by | Suited to | Cost basis |
|---|---|---|---|---|---|
| Coated carbon steel | Barrier film | Holidays, impact damage | DFT and holiday test | Large accessible surfaces within a grade limit | Project-specific |
| Allowance plus coating | Barrier film plus reserve steel | Film damage between inspections | UT, DFT and holiday test | Structural margin on new build or retrofit | Project-specific |
| Solid 316L or higher alloy | Passive film | Chloride pitting and cracking | Visual, pit depth survey | Inaccessible geometry, no outage window | Project-specific |
| Stainless liner or cladding | Metal face over carbon steel | Local penetration, crevices | Visual, pit depth survey | Retrofits with a qualified liner alloy | Project-specific |
| Bare steel with allowance | Sacrificial thickness | Local penetration | UT survey | Dry, above-dew-point, uniform loss | Project-specific |
Coated Carbon Steel with a Matched FlueGard Grade
Coated carbon steel ranks first because it addresses localized condensate attack directly on large steel surfaces.
Suited To
Coated carbon steel suits large, accessible flue gas surfaces such as baghouses, electrostatic precipitators (ESPs), ducts, stacks, flue gas desulfurization (FGD) scrubbers and vessels. Operating and excursion temperatures must sit inside a grade's service limit, and the site must blast to SSPC-SP10 / NACE No. 2 near-white with a profile above 3 mils (75 µm).
What It Is
Protected carbon steel is carbon steel isolated from the gas by an engineered barrier coating. Polylloy matches the grade to the service limit:
- CorrosionGard-160S: 160 °C (320 °F), ambient cure, for structures and vessels.
- FlueGard-225SQC: 225 °C (437 °F), two-component polymeric alloy, immersion-rated.
- StackGard®-255SQW: 255 °C (491 °F), for chimneys, ducts and fans.
- FlueGard-425S: 425 °C (797 °F) with peaks to 500 °C, single-component inorganic polymeric.
- FlueGard-455CHT: 455 °C (850 °F), two-component ceramic.
Key Features
The FlueGard-225SQC bulletin lists resistance to SO3, sulfur dioxide (SO2), hydrogen chloride (HCl), carbon dioxide (CO2), hydrogen fluoride (HF) and nitrogen oxides (NOx). It reports one-week immersion weight gain below 0.5 % in 36 % sulfuric acid (ASTM D471) and pull-off adhesion above 3,000 psi (ASTM D4541).
FlueGard-225SQC also passed Polylloy's own six-month sulfuric acid immersion test in 56 % sulfuric acid at 60 °C without observed deterioration; it is not an independent test.
In the field, at Woodland Biomass Power Plant (Xcel Energy) in California, a previous high-temperature coating and a stainless-steel lining had both been unsuccessful in the baghouse clean-air section. After seven months the FlueGard-225 trial compartment was reported in excellent condition with no corrosion, and the plant asked for the remaining compartments to be coated.
Limits
A coating does not restore lost wall thickness, and a holiday or impact exposes carbon steel to acid, so continuity and repair discipline are part of the design. Heat-cured grades need start-up heat: final heat cured activation is completed during start-up using process heat. Polylloy formulates, supplies, specifies and supervises; certified partners apply the coatings.
Cost Factors
Protected carbon steel may offer a cost-effective alternative to stainless steel where the coating is suitable for the specified service conditions. Cost depends on grade selection, surface preparation and access, area and thickness, labor and inspection, freight and shutdown timing.
Corrosion Allowance Plus Coating on Carbon Steel
Corrosion allowance plus coating combines a barrier with reserve steel.
Suited To
The combination suits new-build structural or pressure-retaining steel where the engineer of record wants structural margin if the film is damaged between inspections. It also suits retrofits where existing steel still has thickness above its design minimum.
What It Is
The coating keeps condensate off the steel, and the allowance is held in reserve. In a retrofit, the remaining existing wall plays the role of the allowance, so measure it by elevation against the structural minimum before coating.
Key Features
The combination has two inspection routes: UT on the steel, and DFT and holiday testing on the coating. What each test proves is set out in the coating standards and tests to ask for. Thinned or perforated plate is repaired before coating, because a coating does not restore wall thickness.
Limits
The allowance value and code basis belong to the engineer of record; Polylloy does not publish allowance figures. Extra thickness adds steel weight and fabrication, and the combination is a design choice rather than a route to a stated life extension.
Solid 316L Stainless or Higher Alloy Construction
Solid 316L stainless or a higher alloy is the right answer where coating is impractical.
Suited To
Upgraded metallurgy suits parts that cannot be blasted, coated or inspected, such as small-bore piping, bellows, complex internals and tight crevices. It also suits service temperatures above every coating grade's limit, and projects with no outage window for surface preparation.
What It is and Its Limits
Upgraded metallurgy relies on a passive chromium-rich film; molybdenum improves 316L's localized resistance relative to 304L but gives no immunity, and chloride condensate can still pit and crack it. Duplex, 904L and nickel alloys each need individual selection, covered in alternatives to 316 stainless steel.
Surjit Gill, Polylloy's co-founder, observes that design teams often specify stainless because it is the known answer. The checklist in the carbon steel vs 316 stainless steel design review tests whether it is the right one.
Cost Factors
Cost is project-specific; compare alloy and coated options on the same equipment, scope and evaluation period.
Stainless Steel Liners and Metallic Cladding Over Carbon Steel
Stainless steel liners and cladding put a corrosion-resistant metal face on existing structural steel.
Suited To
Liners and cladding suit retrofits where a metal face is wanted on existing carbon steel structure and the liner alloy has been qualified for the actual condensate.
What It Is
A liner is a thin stainless sheet, for example a nominal 1 to 2 mm 316L liner, fixed over the structural steel. Cladding is a corrosion-resistant alloy layer bonded to the same base, for example by weld overlay.
Key Features and Limits
Polylloy's technical paper notes that for a nominal 1 to 2 mm 316L liner, local penetration may govern service life rather than average thinning. Increasing thickness adds penetration allowance but does not eliminate pitting or crevice corrosion.
Overlaps, fasteners and deposit-covered areas create shielded crevices that need design attention. At Woodland Biomass, a stainless-steel lining in the baghouse clean-air section had been unsuccessful before the FlueGard trial, though one case does not describe every liner.
Bare Carbon Steel with a Corrosion Allowance Only
Bare carbon steel with a corrosion allowance is the simplest option and fits mild service.
Suited To
Bare steel with an allowance suits steel that stays dry and above the acid dew point in operation and at shutdown, where inspection history shows uniform loss. It also suits short design-life and temporary equipment. A severe-service coating is not needed everywhere, and mild service is better served by simpler protection.
What It Is
The option is uncoated carbon steel thickened by the allowance. Polylloy's technical paper lists carbon steel as requiring a corrosion allowance or effective protection in aggressive condensates.
Limits
In acid condensate the allowance is consumed fastest at the coldest, dirtiest details. Average UT readings can look acceptable while a local area penetrates, so record pit depth and localized damage alongside general thickness.
Evidence a Design Review Needs to Accept Protected Carbon Steel
A design review accepts protected carbon steel on evidence rather than on a material name. Three parts make up the evidence pack.
State the Expected Corrosion Mechanism
Write down whether loss is expected to be uniform or localized, and why. Record conditions at the metal surface: minimum and peak wall temperatures, dew point exposure, deposits, chloride input from fuel changes and shutdown frequency.
Attach Product and Test Evidence with Its Limits
Attach the following evidence, each item stated with its limits:
- Grade bulletin: service limit, chemical resistance (ASTM D471) and adhesion (ASTM D4541 where the bulletin names it). FlueGard-455CHT lists Elcometer adhesion above 1,000 psi (7 MPa), with no test standard named.
- Test reports: the 56 % sulfuric acid report is Polylloy's own and covers one concentration and one temperature.
- Woodland Biomass baghouse: no corrosion in the trial compartment after seven months.
- Taipower 12-month FGD field trial on FlueGard-225 coupons: no measurable loss of coating thickness, pull-off adhesion above 1,300 psi with failure in the dolly adhesive, and a 2 kV holiday test passed.
- FlueGard on three coal mill baghouses at cement plants in Mexico, inspected after about 15 to 20 years.
Commit to an Inspection Plan
Define the quality plan at application (SSPC-SP10, profile, DFT, holiday test) and in service (coating condition, UT on any allowance). Polylloy's technical team provides project-specific performance detail for the review.
How to Choose Between Corrosion Allowance, Coating and Metallurgy
Choosing between a corrosion allowance, a coating and upgraded metallurgy follows five rules:
- Dry, above-dew-point service with uniform loss: an allowance alone or a conventional coating.
- Acid or chloride condensate on large accessible steel inside a grade's limit: coated carbon steel.
- Structural margin wanted on new build: allowance plus coating.
- Inaccessible geometry, no blast or outage window, or temperatures above every grade: 316L or a higher alloy.
- Liners only with the alloy qualified for the condensate and crevice details designed out.
Compare cost on the same equipment, scope and period as material, installed and lifecycle cost. Lifecycle evaluation considers preparation, application, maintenance, downtime and replacement alongside the initial material cost, as set out in industrial coating project cost.
The grades are described on the FlueGard flue gas coatings page. To test a design basis, request a coating evaluation with equipment type, coated area, operating conditions (temperature, gas chemistry, abrasion), location and outage timing.
FAQs
What is a Corrosion Allowance?
A corrosion allowance is extra wall thickness added to steel beyond what strength requires, intended to be consumed by corrosion over the design life. It works when metal loss is predictable and reasonably uniform. The value and its code basis are set by the designer or engineer of record for the specific equipment and service conditions.
Is a Corrosion Allowance Enough for Steel in Acid Gas Service?
Often not on its own, because acid condenses where steel runs below the acid dew point, at cold spots, air leaks and under deposits, so loss concentrates locally. An allowance sized on average loss can be consumed at one detail while the rest of the wall looks sound. Pair it with protection or confirm loss is uniform.
Can a Coating Replace a Corrosion Allowance on Carbon Steel?
A coating changes the design approach: it keeps condensate off the steel instead of sacrificing thickness. Whether any allowance is still specified is the engineer of record's decision. A coating does not restore lost wall thickness, so existing thinned plate is repaired first, and film continuity is verified with DFT and holiday testing.
How Do You Justify Protected Carbon Steel to a Design Review?
Bring evidence, not a material name. State the expected corrosion mechanism and conditions at the metal surface, then attach the grade bulletin's service limit and chemical resistance data, test reports with their limits, field references in comparable service and an inspection plan. Polylloy's technical team supplies project-specific performance detail for the review.
Should We Coat the Carbon Steel or Upgrade to 316 Stainless?
Coat when surfaces are large and accessible, temperatures sit inside a grade's service limit and the site can blast to SSPC-SP10 near-white. Upgrade to 316L or a higher alloy when parts cannot be blasted, coated or inspected, or exceed every coating limit. Chloride condensate can still pit 316L, so qualify either choice.
Does a Thicker Stainless Steel Liner Stop Pitting?
No. Polylloy's technical paper notes that for a nominal 1 to 2 mm 316L liner, local penetration may govern service life rather than average thinning. Extra thickness adds penetration allowance but does not remove pitting or crevice corrosion, and overlaps, fasteners and deposits create shielded crevices that need design attention.
Edita Rojasova
Co-founder and Chief Technology Officer, Polylloy Coatings
Edita Rojasova is co-founder and Chief Technology Officer of Polylloy Coatings, Inc., which develops hybrid polymer-alloy-ceramic technologies that protect industrial equipment in extreme environments against high-temperature corrosion, chemical attack, and abrasion. A materials scientist educated at the Slovak University of Technology in Bratislava, she holds a master’s degree in chemical engineering and fuel processing and a PhD in organic technology, with a focus on catalysis and the modification of inorganic substrates. She brings expertise in both organic and inorganic chemistry, integrating the two into true hybrid protective systems. Her specializations include electrochemistry, corrosion mechanisms of metallic substrates, and the chemistry of the substrate–coating interface. An inventor with multiple U.S. patents, she leads Polylloy’s R&D, guiding new formulations from testing and characterization through to field implementation.
Related Signals
7 Design Rules to Prevent Acid Condensation in Flue Gas Ductwork
Edita RojasovaSun, Oct 25, 2026
Flue Gas Composition: 7 Components and the Corrosion Each Causes
Edita RojasovaSat, Oct 24, 2026