Why 316 Stainless Steel Corrodes in Acidic Flue Gas
 Surjit GillLast Updated: Oct 6, 2026
316 Stainless Corrosion in Flue Gas: Key Points
- 316 relies on a thin chromium oxide passive film, and acidic, reducing or chloride-rich condensate breaks it down.
- Below the acid dew point, sulfuric acid condenses on cold metal and can corrode 316 actively at some acid concentrations and temperatures.
- Chlorides from fuel, including alternative fuels, concentrate in condensate and deposits, causing pitting, crevice corrosion and chloride stress corrosion cracking.
- Cold spots, air in-leakage, hygroscopic deposits, start-stop cycling and poorly finished welds accelerate attack.
- Diagnose with metal temperature mapping, condensate and deposit analysis, and pit and crack examination before changing material.
- Options: remove cold spots, step up to a higher alloy, or protect carbon steel with a coating matched to the temperature and chemistry.
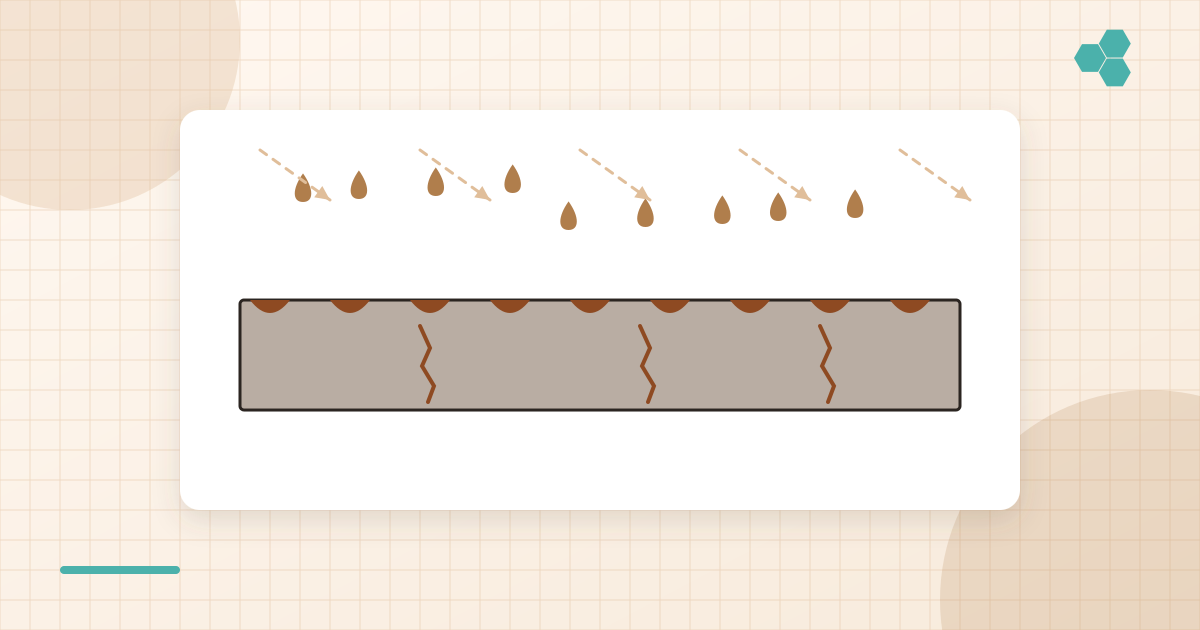
316 stainless steel corrodes in acidic flue gas because condensate forming below the acid dew point, often loaded with chlorides, breaks down the chromium oxide passive film that normally protects it. Sulfuric acid causes general attack at susceptible concentrations, while chlorides cause pitting, crevice corrosion under deposits and chloride stress corrosion cracking at welds. Cold spots and start-stop cycling make every one of these worse.
The practical consequence is that 316 is not automatically the safe specification for flue gas. Whether it is necessary, adequate or inadequate depends on where condensate forms, what it carries and how the equipment is detailed, which is what the rest of this guide helps you establish.
How 316 Stainless Protects Itself and What Breaks the Passive Film
316 stainless protects itself with a passive film, a very thin chromium oxide layer that forms spontaneously on the surface. Molybdenum, the main alloying addition that distinguishes 316 from 304, makes that film more resistant to chloride pitting. The film is not a coating: it is part of the metal surface, and it heals itself only when the environment is oxidizing enough to rebuild it.
Reducing acids, low-pH condensate and chloride ions attack the passive film faster than it can repair. Once the film breaks down locally, the bare alloy underneath has no second line of defense at that spot. That is why "stainless" means stain-resistant in many environments, not immune in all of them, and why flue gas condensate is one of the environments where the distinction matters.
Acid Dew Point Corrosion: Why Condensing Sulfuric Acid Attacks 316
Acid dew point corrosion begins with the fuel. Sulfur burns to sulfur dioxide (SO2) and a smaller fraction of sulfur trioxide (SO3); the SO3 combines with water vapor and condenses as sulfuric acid on any surface colder than the acid dew point.
The acid strength in that condensate film changes with metal temperature, so neighboring spots on the same duct can see quite different acid concentrations. 316 does not reliably resist this. Published iso-corrosion charts for 316 in sulfuric acid show a window of concentration and temperature where the alloy corrodes actively, and condensate in flue gas equipment can fall inside it.
The honest answer to "does stainless resist sulfuric acid dew point corrosion" is that 316 resists some conditions but not all, so dew point service needs an engineering check against that data rather than an assumption.
In practice the attack concentrates where metal runs cool: duct walls near air in-leakage, expansion joints, dampers, hopper walls, outlet plenums, uninsulated stiffeners and stack tops. Every start-up and shutdown also takes the whole surface through the dew point, so cycling units collect condensate exposure even when steady-state temperatures look safe.
Chloride Attack: Pitting, Crevice Corrosion and Stress Corrosion Cracking in 316
Chloride attack on 316 starts with chlorine in coal, waste, biomass and alternative fuels, which forms hydrogen chloride (HCl) in the flue gas. The HCl dew point sits below the sulfuric acid dew point, so hydrochloric acid condenses at colder spots and in shutdown condensate.
Chloride salts in fly ash and kiln dust also settle on metal surfaces, and plants that raise alternative-fuel rates often see this load change.
Pitting and Crevice Corrosion
Pitting begins where chlorides concentrate and break the passive film at individual points. Inside a pit the chemistry turns more acidic and chloride-rich as the metal dissolves, so the pit drives its own growth. Crevices under deposits, gaskets, lap joints and bolted connections develop the same chemistry faster, and pits can perforate thin walls while the surrounding surface still looks sound.
Chloride Stress Corrosion Cracking
Chloride stress corrosion cracking needs three conditions at once: chlorides, tensile stress and elevated metal temperature. Flue gas equipment can supply all three, with weld residual stress, fit-up stress and thermal stress providing the tension. Austenitic grades including 316 are susceptible, and the cracks are typically branched and mainly transgranular, running through the grains and often found right beside welds.
Deposits, Cycling and Welds Accelerate Attack on 316
Hygroscopic deposits are a large part of why 316 fails faster than steady-state conditions suggest. Chloride and sulfate deposits absorb moisture from air during outages and form a corrosive film on the metal while the unit is offline. Frequent start-stop operation multiplies dew point crossings, so a unit that cycles often accumulates far more wet exposure than one that runs continuously.
Weld zones are the second accelerator: heat tint left unpickled lowers local corrosion resistance, and standard-carbon 316 can sensitize in the heat-affected zone, where chromium carbides form at grain boundaries and strip chromium from the adjacent metal. 316L, the low-carbon version, reduces sensitization but does not improve chloride pitting resistance. Weld residual stress then supplies the tension that chloride stress corrosion cracking needs.
How to Diagnose Which Mechanism is Attacking Your 316 Equipment
Diagnosing corroded 316 before choosing a fix avoids replacing like with like and getting the same result. In flue gas service, the failure pattern usually tells you the mechanism once it is mapped against temperature and chemistry. Three steps cover most cases.
Map Metal Temperatures Against Dew Points
Survey skin temperatures with thermography and contact probes during normal running, low load and start-up, then mark areas below the sulfuric acid and HCl dew points. Check doors, joints and expansion joints for air in-leakage, which creates local cold spots.
Analyze Condensate and Deposits
Sample deposits and condensate for pH, chloride, sulfate and fluoride, and note any change after fuel switches. A chloride-dominated result usually points to pitting and cracking; a sulfate-dominated, low-pH result usually points to acid dew point attack.
Examine the Damage
Compare pit morphology and location, under deposits or at crevices, with the crack pattern found by dye penetrant testing at welds. A metallographic section separates branched transgranular cracking (chloride stress corrosion cracking) from intergranular attack at sensitized welds. Record wall loss by ultrasonic thickness testing to judge the remaining life of existing 316.
If coated carbon steel is chosen, the coating then needs its own condition checks; Polylloy's inspection and maintenance services page outlines visual, film thickness and adhesion inspection.
Options When 316 is Not Holding Up in Flue Gas
Options for failing 316 fall into three groups, and the diagnosis decides which fits. Many plants combine the first with one of the other two.
Remove the Cold Spots
Insulation repairs, heat tracing, sealing air in-leakage and better start-up and shutdown purges address the cause directly. They reduce condensation during operation but cannot fully prevent shutdown condensate on deposits.
Step Up the Alloy
Duplex, super-austenitic and nickel-chromium-molybdenum alloys offer higher chloride resistance. The Pitting Resistance Equivalent Number (PREN), calculated from chromium, molybdenum and nitrogen content, ranks resistance to chloride pitting but not to acid attack or stress corrosion cracking. Higher alloys still need selection for the actual condensate, and their fabrication is more demanding.
Protect Carbon Steel with a Matched Coating
A barrier coating on carbon steel takes the passive-film mechanism out of the equation. Polylloy grades are matched by service limit:
- FlueGard®-225SQC: 225 °C (437 °F)
- StackGard®-255SQW: 255 °C (491 °F)
- FlueGard-425S: 425 °C (797 °F), with spikes to 500 °C (932 °F)
- FlueGard-455CHT: 455 °C (850 °F), with good resistance to acidic and alkaline condensates
Chemistry selection matters, because Polylloy laboratory and field testing observed undercutting corrosion and delamination in conventional high-temperature coatings. Polylloy's certified application partners apply the coating under Polylloy supervision; surface preparation is critical, and any damage must be repaired. Grade details are on the FlueGard flue gas coatings page.
Is 316 Necessary for Your Flue Gas Application? A Decision Path
316 is necessary only when the conditions call for it and a better-matched option does not exist. Where there is no acidic condensate and chloride levels are low, 316 or even plain carbon steel may be adequate. Where acidic chloride condensate forms, 316 is at risk, so compare a higher alloy with protected carbon steel on a like-for-like basis.
The same like-for-like logic applies to every flue gas asset, from baghouses to stacks, and Polylloy's corrosion protection solutions are matched to each by service limit. Request a coating evaluation with equipment type, area, operating conditions, location and timing.
FAQs
Does 316 Stainless Steel Resist Sulfuric Acid Dew Point Corrosion?
Only partly. 316 resists some sulfuric acid conditions but corrodes actively at certain acid concentrations and metal temperatures, and condensate strength varies from spot to spot as metal temperature changes. Any surface running below the acid dew point, including during start-ups and shutdowns, needs an engineering check against iso-corrosion data rather than an assumption that stainless is enough.
Why Does 316 Stainless Corrode in Acidic Chloride Condensate?
Chloride ions break down the chromium oxide passive film locally, and the acidic condensate stops it from healing. Corrosion then concentrates at points, forming pits, and inside crevices under deposits, gaskets and lap joints. Where tensile stress and elevated temperature are also present, typically near welds, the same chlorides can cause stress corrosion cracking.
Can 316 Stainless Steel Suffer Chloride Stress Corrosion Cracking in a Flue Gas Duct?
Yes: chloride stress corrosion cracking needs chlorides, tensile stress and elevated temperature together, and ducts can supply all three: chloride-bearing condensate or deposits, weld residual stress and warm metal. Cracks are typically branched and run through the grains, often beside welds. Dye penetrant testing and metallographic sections confirm the mechanism.
Is 316L Better Than 316 in Flue Gas Service?
316L helps at welds but not against chlorides. Its lower carbon content reduces sensitization in the weld heat-affected zone, which limits intergranular attack. It does not raise resistance to chloride pitting, which depends on chromium, molybdenum and nitrogen, or to chloride stress corrosion cracking, which depends mainly on nickel content, stress and temperature.
Will a Higher Alloy Solve Corrosion Where 316 Failed?
It can, if the alloy is selected for the actual condensate. Duplex, super-austenitic and nickel-chromium-molybdenum alloys resist chlorides better than 316, but each has its own limits in strong acid. Confirm temperatures, condensate chemistry and deposit composition first, then compare the higher alloy with protected carbon steel on a like-for-like lifecycle basis.
Can a Coating Protect Equipment Where 316 Stainless Has Corroded?
Yes, usually by replacing failed sections with coated carbon steel, which avoids the passive-film mechanism, provided the grade suits the temperature and chemistry. Polylloy grades include FlueGard-225SQC to 225 °C, FlueGard-425S to 425 °C and FlueGard-455CHT to 455 °C. Coating existing stainless surfaces is a separate question for Polylloy's technical team.
Surjit Gill
Co-founder, Polylloy Coatings
Surjit Gill is co-founder of Polylloy Coatings, which develops innovative hybrid coatings to protect industrial equipment against high-temperature corrosion, chemical attack, and abrasion in severe-service applications worldwide. Trained in chemical engineering and business management, he brings leadership experience spanning startup incubation and business growth. He focuses on commercializing materials innovation, scaling organizations, and advancing go-to-market strategy through global partnerships.
Related Signals
Corrosion Behind Refractory Linings: How to Protect the Steel
 Edita RojasovaThu, Sep 24, 2026
How to Choose an Industrial Coating Company for Severe Service
Edita RojasovaWed, Sep 2, 2026